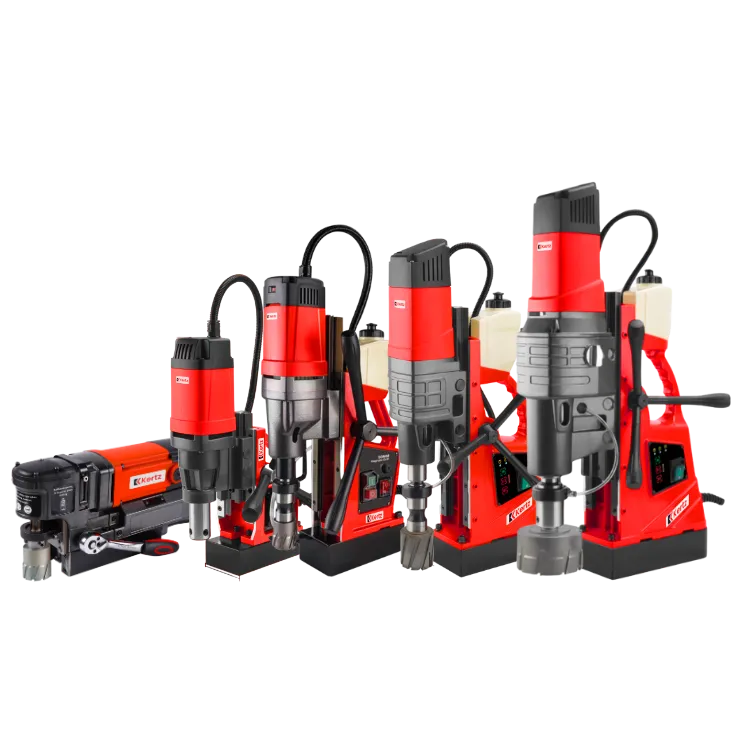
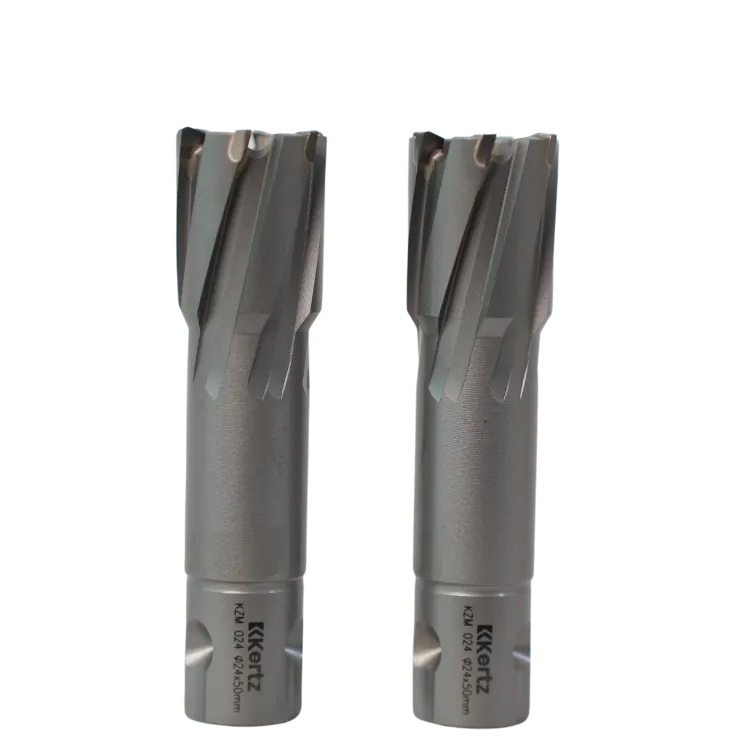
Magnetic Drill & Annular Cutter Maintenance for Long Life and Accuracy
Magnetic drill and annular cutter maintenance: daily checks, slide lubrication, carbon brushes, magnet base, coolant, cutter storage, and troubleshooting.
Avenix Team
· 6 min read
 Ilustrasi
Summary
Most magnetic drill and annular cutter failures come from a dirty magnet base, a loose slide, too little coolant, and the wrong speed or feed pressure. Clean and check the machine daily, adjust and lubricate the slide regularly, replace carbon brushes before they wear out, always use cutting oil, and store cutters in their cases.
Magnetic drills and annular cutters last longer and stay accurate when the magnet base is kept clean, the slide is adjusted and lubricated, carbon brushes are replaced on time, coolant is always used, and cutters are stored properly. Most broken cutters, oversized holes and machines slipping off the workpiece can be prevented with simple routine maintenance.
This guide is for operators, workshop leads and maintenance teams in fabrication workshops, shipyards and structural steel projects. If you are still choosing equipment, read how to choose an annular cutter and magnetic drill first.
Always follow your machine manufacturer’s manual. Unplug the machine before cleaning, adjusting or replacing parts.
Daily checks before use
| Component | What to check |
|---|---|
| Cable and plug | Not cut or kinked, plug not loose or scorched |
| Magnet base | Flat, free of chips, weld scale and rust |
| Magnet and motor switches | Work independently, magnet engages with a firm hold |
| Safety chain or strap | Present, intact and fitted before drilling |
| Slide and feed handle | Moves smoothly with no side play |
| Arbor and cutter holder | Clean, locking screws not damaged |
| Coolant system | Tank filled, tap and hose not leaking or blocked |
| Chip guard | Fitted |
Magnetic drill maintenance
1. Magnet base
Magnetic holding force depends on full contact between the base and the workpiece.
- Clean the base of metal chips after every use. Small chips stuck to it create a gap and reduce holding force.
- Check the base is flat. Deep scratches or raised burrs from knocks can be dressed with a flat stone, but a base that is no longer flat should be repaired by an authorised technician.
- Prepare the workpiece surface: flat and free of thick paint, rust and weld scale. On thin plate, add a steel plate under the magnet area.
2. Slide and gib
A loose dovetail slide makes the cutter vibrate, enlarges the hole and chips cutter teeth.
- Adjust the gib screws evenly until the slide moves smoothly with no side play. Over-tightening makes feeding heavy.
- Lubricate the slide and feed rack regularly with the lubricant the manufacturer recommends, and clean off chips.
3. Motor and carbon brushes
Many magnetic drills use motors with carbon brushes.
- Check carbon brush length on the schedule in the manual, and replace both brushes together before they reach the wear limit.
- Excessive sparking around the commutator, a burning smell or a motor that stutters are signs of worn brushes or a dirty commutator.
- Keep motor vents clean so the motor does not overheat.
4. Arbor and run-out
A bent arbor or dirty holder makes the cutter spin off-centre (run-out), so holes come out oversized and the cutter wears quickly.
- Clean the holder and cutter shank before fitting.
- Tighten the locking screws onto the flats of the Weldon shank.
- If holes are consistently oversized or the cutter vibrates even with the slide adjusted, have the arbor and bearings checked.
5. Cables and electrics
- Never drag the machine by its cable.
- Use extension cables with an adequate cross-section, as voltage drop can weaken both magnet and motor.
- Avoid coiling the cable too tightly or running heavy equipment over it.
6. Coolant system
- Clean the tank and hose of sediment and chips regularly.
- Make sure coolant flows through the pilot pin to the cutting zone.
- Empty the tank if the machine will be stored for a long time so the coolant does not settle.
Annular cutter maintenance
1. Use coolant correctly
Coolant cools the teeth, lubricates the cutting surfaces and helps clear chips. Use cutting oil or a water-soluble metalworking coolant. Do not use used oil or plain water. For vertical or overhead drilling, use a cutting paste or oil that clings.
2. Correct speed and feed pressure
- Larger diameters need lower spindle speeds. Follow the speed tables from the cutter and machine manufacturers.
- Start with light pressure until the teeth bite, then apply steady pressure until breakthrough.
- Long, curly, silver chips indicate good parameters. Dark blue or powdery chips indicate excess heat or a blunt cutter.
3. Pilot pin and spring
- Check the pilot pin for bending and wear, and make sure the spring still ejects the slug.
- Use a pilot pin of the correct diameter and length for the cutter. In the Kertz range, for example, different pilot pins are available for 35 mm and 50 mm depth cutters.
4. Clean and store
- Clear chips from inside the cutter and its flutes after use.
- Store cutters in a case or rack so the teeth do not knock against other tools.
- Apply a little anti-rust oil if cutters will be stored for a long time, especially in humid coastal environments.
5. When to resharpen or replace
- Blunt HSS cutters can be resharpened with a dedicated machine and jig to keep the correct tooth angles.
- TCT cutters require carbide sharpening.
- Replace cutters with several chipped teeth, cracks or a bent body.
Quick troubleshooting
| Problem | Likely cause | Action |
|---|---|---|
| Machine shifts or releases while drilling | Dirty magnet base, thin plate, rusty or heavily painted surface, voltage drop | Clean base and surface, add a plate under the magnet, check cable and power supply |
| Chipped cutter teeth | Loose slide, too much initial pressure, magnet not flat | Adjust gib, light initial pressure, check magnet contact |
| Oversized hole | Arbor run-out, loose slide, cutter not seated properly | Clean and tighten cutter, adjust slide, check arbor |
| Slug stuck | Bent pilot pin, weak spring, chip build-up | Replace pilot pin or spring, clean cutter |
| Cutter blunts quickly | Not enough coolant, speed too high, hard material | Increase coolant, reduce speed, consider a TCT cutter |
| Motor hot or stuttering | Worn carbon brushes, blocked vents, overload | Replace brushes, clean vents, reduce feed pressure |
Maintenance schedule summary
| Frequency | Action |
|---|---|
| Every use | Check cable, clean magnet base, fit safety chain, fill coolant |
| End of every shift | Clean chips from machine and cutter, store cutter in its case |
| Weekly | Check and adjust slide, lubricate slide and feed rack |
| Monthly or per manual | Check carbon brushes, clean coolant tank, check pilot pin and spring |
| Yearly | Full service by a technician, including electrical insulation testing |
Conclusion
Maintaining magnetic drills and annular cutters is not complicated, but it must be routine: a clean magnet base, a slide with no play, monitored carbon brushes, coolant every time, and the right speed and pressure. These habits extend cutter life, keep holes accurate and reduce the risk of accidents.
Avenix supplies Kertz magnetic drills such as the KMD-35 and KMD-60X, TCT annular cutters in the KZS 35 mm and KZM 50 mm series, and pilot pins for workshops in Batam and Bintan. Browse the magnetic drills and annular cutters categories, use the annular cutter selector, or send your requirements via Request a Quote.